Deep drawing is not a process where the lowest quote wins. A supplier who skips draw simulation, treats wall thinning as a “final inspection issue,” or cannot tell you the temper of the blanks they are running will cost you far more in scrapped parts, die rework, and missed launches than the few cents per piece you thought you saved.
This guide is written for OEM buyers and engineers who need a deep drawing partner, not just a price list. Below are seven checks that actually predict whether your project will run smoothly — and what to have ready so you can get an accurate quote back within 24 hours.
Check 1: Material Selection Follows a Fixed Sequence, Not Guesswork
The most common deep drawing mistake happens before a die is ever cut: the material is chosen for its end-use property first, and its formability second. A part needs corrosion resistance, so stainless steel is specified — and then the geometry cannot be drawn without multiple annealing steps that double the cost.
Reliable suppliers reverse the sequence:
Can the material form the shape? Deep drawing demands ductility. Low-carbon steel (DC04, DC06) draws more forgivingly than 304 stainless, which work-hardens quickly and is prone to galling.
Does it meet the functional requirement? Magnetic response, corrosion resistance, conductivity, or weight.
Does the total cost make sense? Stainless steel may eliminate a plating step, but its material price, slower draw cycles, and faster die wear can push total cost to two or three times that of carbon steel.
A supplier who asks about draw ratio and material temper before quoting a price is already ahead of the field.
Check 2: Draw Simulation Happens Before Tooling Is Cut
This is the single strongest signal of a supplier’s technical maturity. Finite Element Analysis (FEA) simulates the forming process digitally and predicts wrinkling zones, tearing risks, and wall-thinning locations before a single piece of tool steel is machined.
A supplier without simulation is guessing — and your tooling budget absorbs the risk. Ask directly: “Will you provide a draw simulation report before tooling approval?” If the answer is “we’ll adjust on the press,” treat that as a red flag.
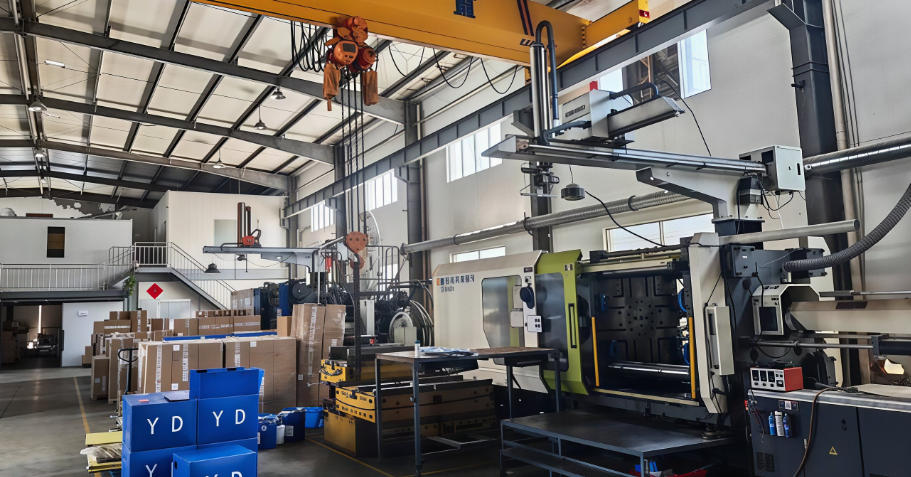
Check 3: In-Process Thickness Mapping, Not Just Final Inspection
Deep drawing defects develop gradually. A die wears down over thousands of strokes; wall thinning worsens incrementally. Inspecting only at the end of a run means thousands of non-conforming parts may already be boxed.
A controlled process includes ultrasonic thickness mapping at 12 or more radial points per part, taken at defined intervals (for example, every 500 parts or at each coil change), with acceptance criteria tied to the drawing tolerance — typically ±5% of nominal wall thickness. Spot-checking two or three points can miss localized thinning caused by uneven lubrication or die wear.
Check 4: Die Maintenance Is Documented, Not Assumed
Dies are not permanent. Wear on the draw ring and punch radius directly affects wall thickness and surface quality. A supplier who cannot show die maintenance records is asking you to trust memory over measurement.
Look for wear measurements logged at fixed stroke intervals — every 5,000 strokes is a workable benchmark — along with die hardness checks and records of when inserts or rings were replaced. Vague verbal assurances are not traceability.
Check 5: Certifications Are Verified, Not Just Printed on the Website
ISO 9001:2015 is the baseline quality management standard. IATF 16949 matters if your part goes into automotive programs, but it is only meaningful if the supplier is actually audited against it and supplies automotive OEMs.
Ask for the certificate number and verify it on the issuing body’s public registry. Confirm that the certified scope covers metal stamping or deep drawing at the same factory address you are dealing with — not a parent company or a different plant.
Check 6: The Quote Is Broken Down, Not Bundled
A credible deep drawing quote separates material, tooling, and processing. This is not just good accounting — it tells you where the cost drivers are and whether the supplier has a realistic understanding of your part.
Tooling cost for deep drawing is a real capital expense: a single-stage die for a relatively simple drawn part may start in the low thousands of dollars, while multi-stage or progressive tooling for complex hollow geometries can run $15,000 to $50,000 or more depending on size and number of stations. A supplier who cannot explain the tooling route — single-hit, transfer, or progressive — is not in a position to quote responsibly.
Check 7: The RFQ Is Complete Before the Clock Starts
The “24-hour quote” promise only works when the input is complete. For a deep drawing quotation that is accurate rather than optimistic, send:
2D drawing (PDF) with critical dimensions and tolerances
3D model (STEP/STP preferred)
Material grade, temper, and thickness
Surface finish and any secondary operations required
Prototype or annual demand quantity
Any traceability or documentation requirements (material certificates, PPAP, etc.)
A supplier who can turn that package around within one business day is telling you something about their engineering capacity — and their confidence in their process.
Where Hony Tai Fits
Hony Tai is built for customized metal structural components, with deep drawing sitting alongside metal stamping, sheet metal fabrication, and precision machining under one roof. That combination matters for drawn parts, because secondary operations — trimming, threading, finishing, assembly — do not disappear into an outsourced supply chain.
We work from customer drawings and samples, develop both standard and non-standard hardware parts, and control precision and production quality through the full process. If you have a deep-drawn housing, cap, shell, or enclosure in mind, send your drawing and requirements. You will receive a quote within 24 hours — with material and tooling logic you can actually evaluate.
Send your RFQ now for a free quote in 24 hours.